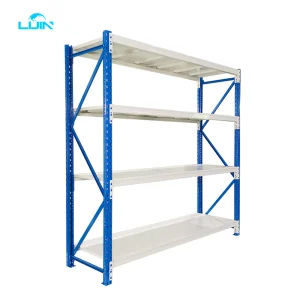
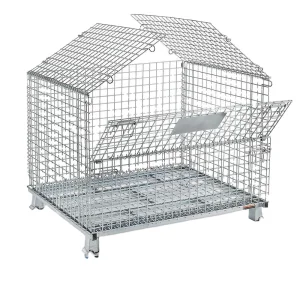
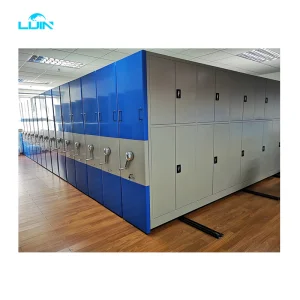
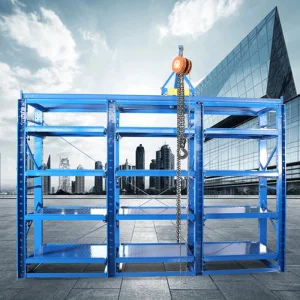
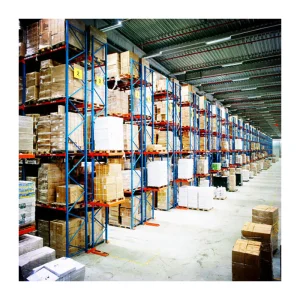
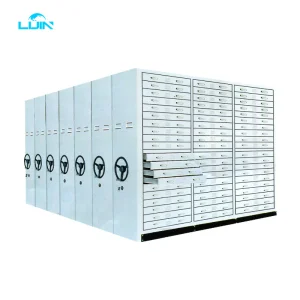
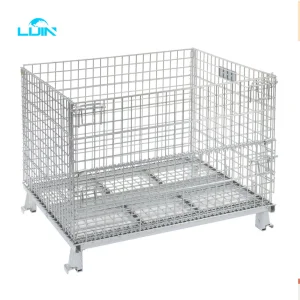
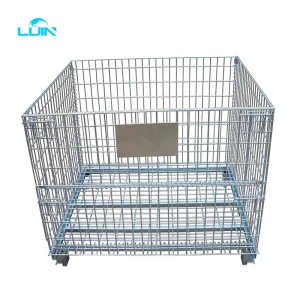
Explore our premium selection of hot sale industrial storage systems, engineered for maximum durability, space optimization, and seamless operational flow.
An authoritative whitepaper on sourcing industrial storage systems from top-tier Chinese manufacturers, optimizing logistics ROI, and scaling supply chain infrastructure.
In the rapidly evolving landscape of global logistics and e-commerce fulfillment, warehouse equipment selection acts as the foundational pillar of operational efficiency. As international enterprises face surging labor costs and space constraints, partnering directly with specialized China wholesale warehouse equipment factories and exporters provides a strategic competitive advantage. Chinese manufacturing excellence—exemplified by industry leaders like Shenzhen Lijin Storage Equipment Co., Ltd.—delivers high-performance structural steel solutions combining cost efficiency, rigorous load testing, and custom engineering.
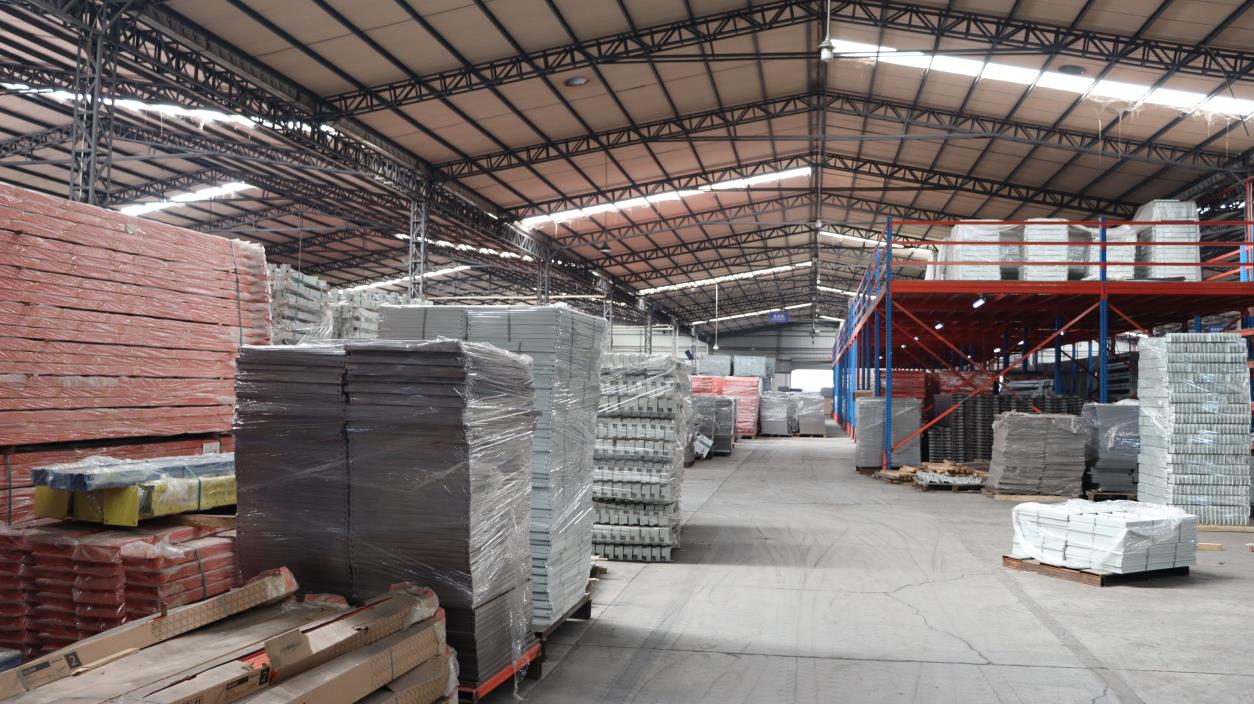
Established in 2015, we are a leading enterprise specializing in the design, manufacturing, and global distribution of heavy-duty warehouse racking systems, automated storage solutions, and industrial shelving.
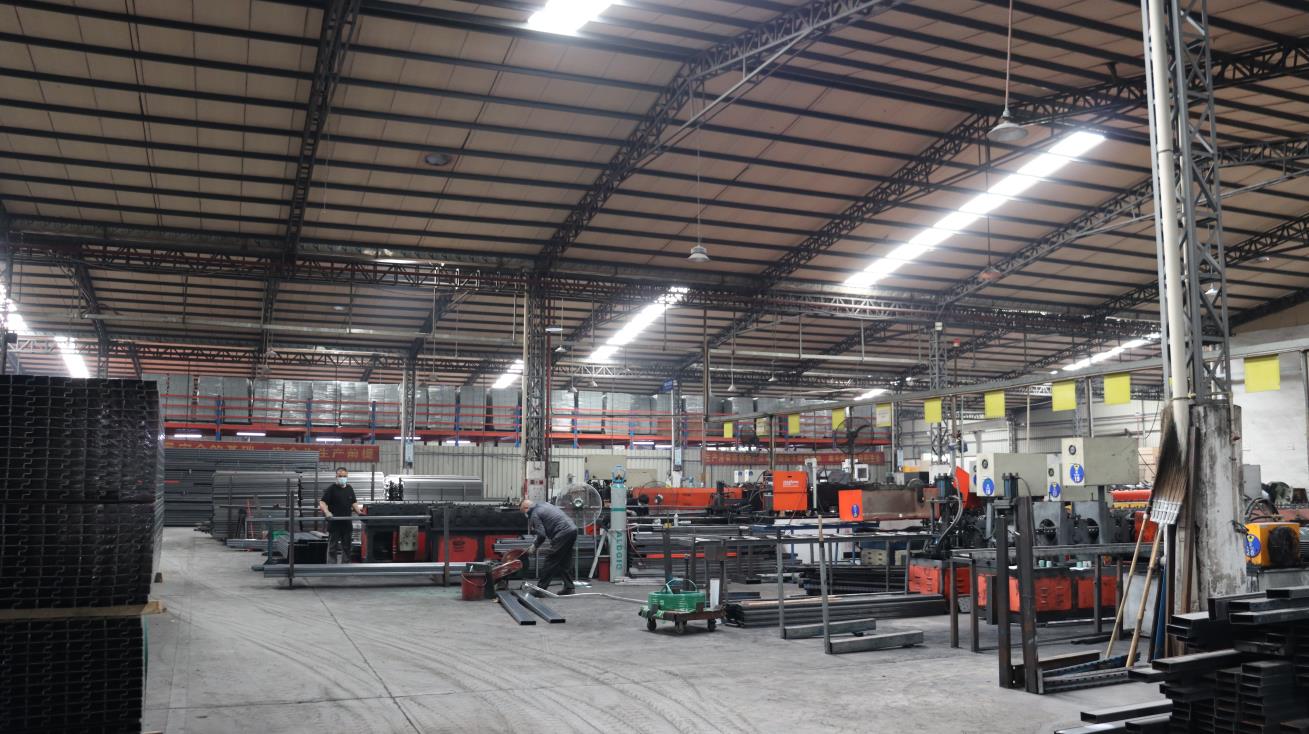
Spanning a state-of-the-art facility of 35,000 m², we have developed into a trusted global supply chain partner with over 8 years of direct export experience and more than 12 years of deep industry expertise. Driven by innovation and quality, our global revenue reached USD 22 million last year.
Our core markets span North America, Western Europe, Southeast Asia, and the Middle East, serving large-scale logistics hubs, commercial distributors, third-party logistics (3PL) providers, and industrial equipment wholesalers.
Supported by a skilled team of 28 R&D engineers, Shenzhen Lijin delivers comprehensive OEM and ODM solutions tailored to unique warehouse layouts, seismic requirements, and capacity needs.
Our engineering team launched over 85 new products and dynamic storage configurations last year, continuously setting new standards in space optimization and modern automated storage integration.
We enforce a rigorous, multi-stage quality control system—including ultrasonic non-destructive testing, automated weld inspection, laser dimensional checking, and heavy-load endurance testing. Backed by an in-house quality inspection team of 35 dedicated professionals, every batch meets international safety and structural standards, ensuring maximum load-bearing efficiency and long-term stability.
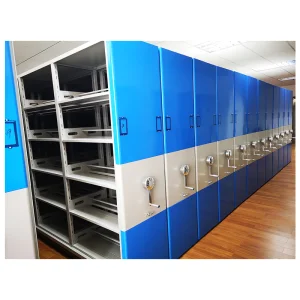
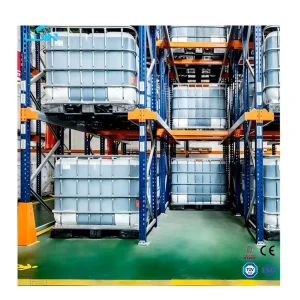
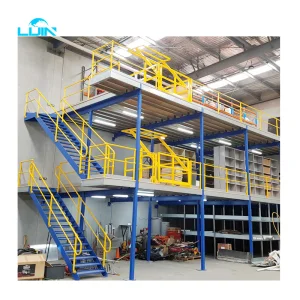
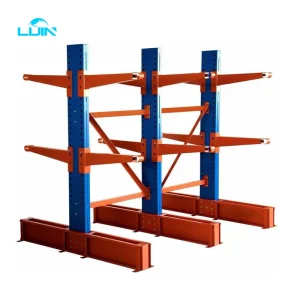
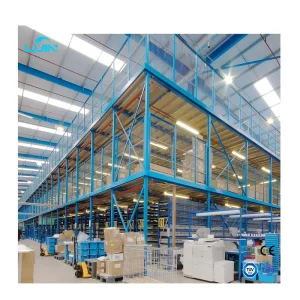
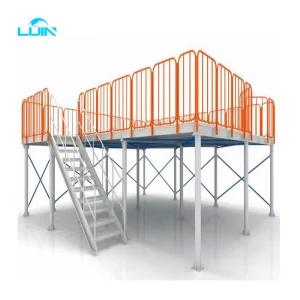
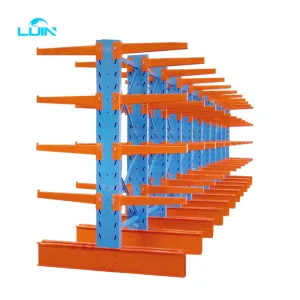
Discover our heavy-duty platforms, mezzanine floors, customized cantilever racks, and mobile compactor solutions built for extreme industrial conditions.
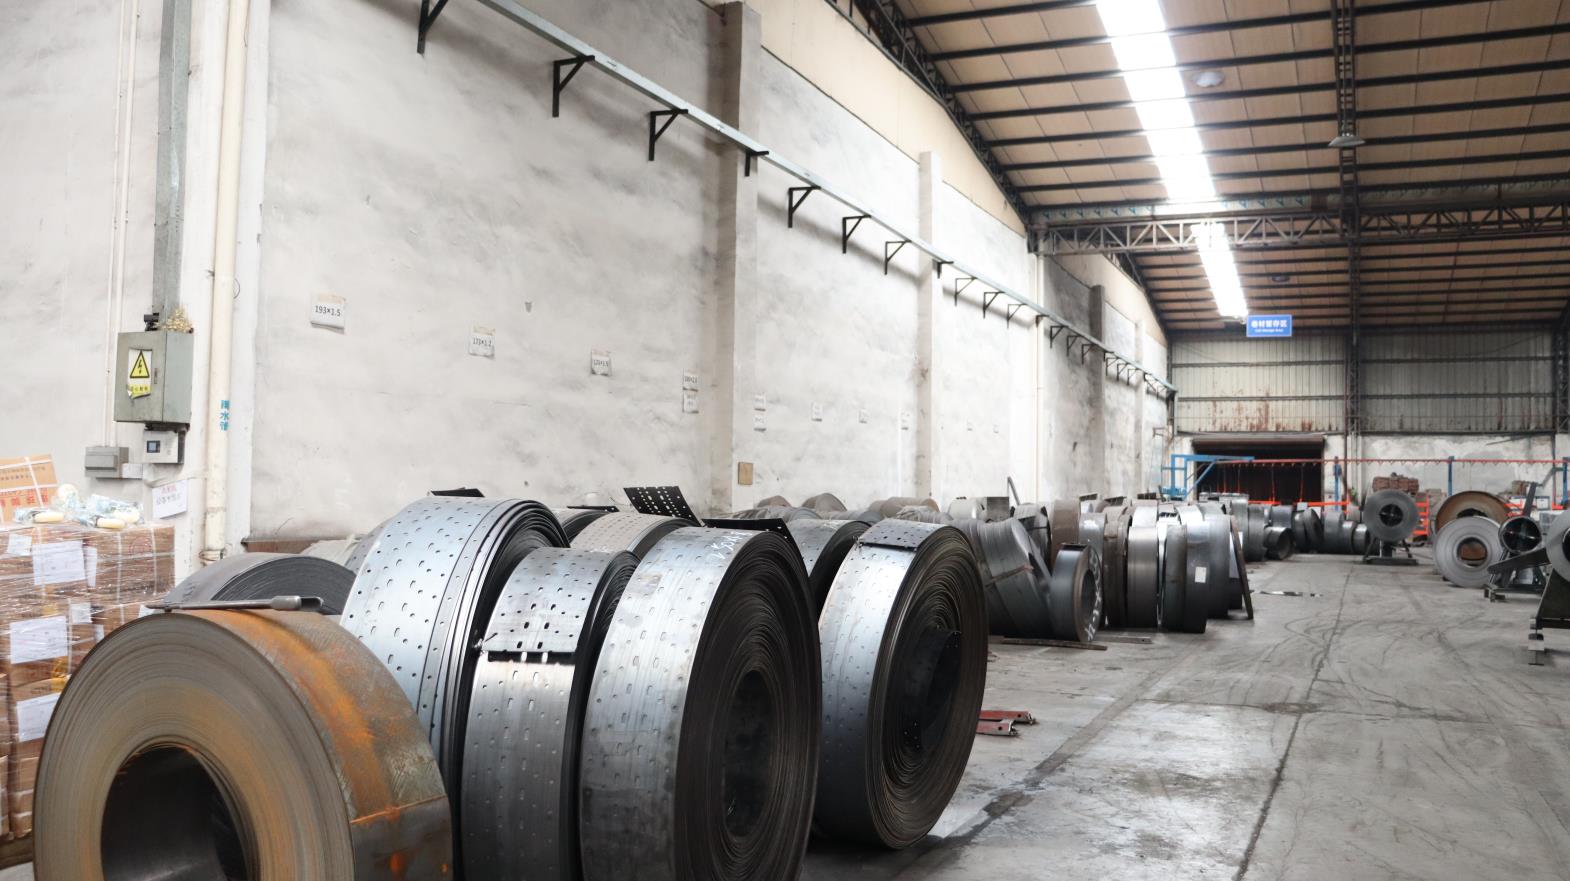
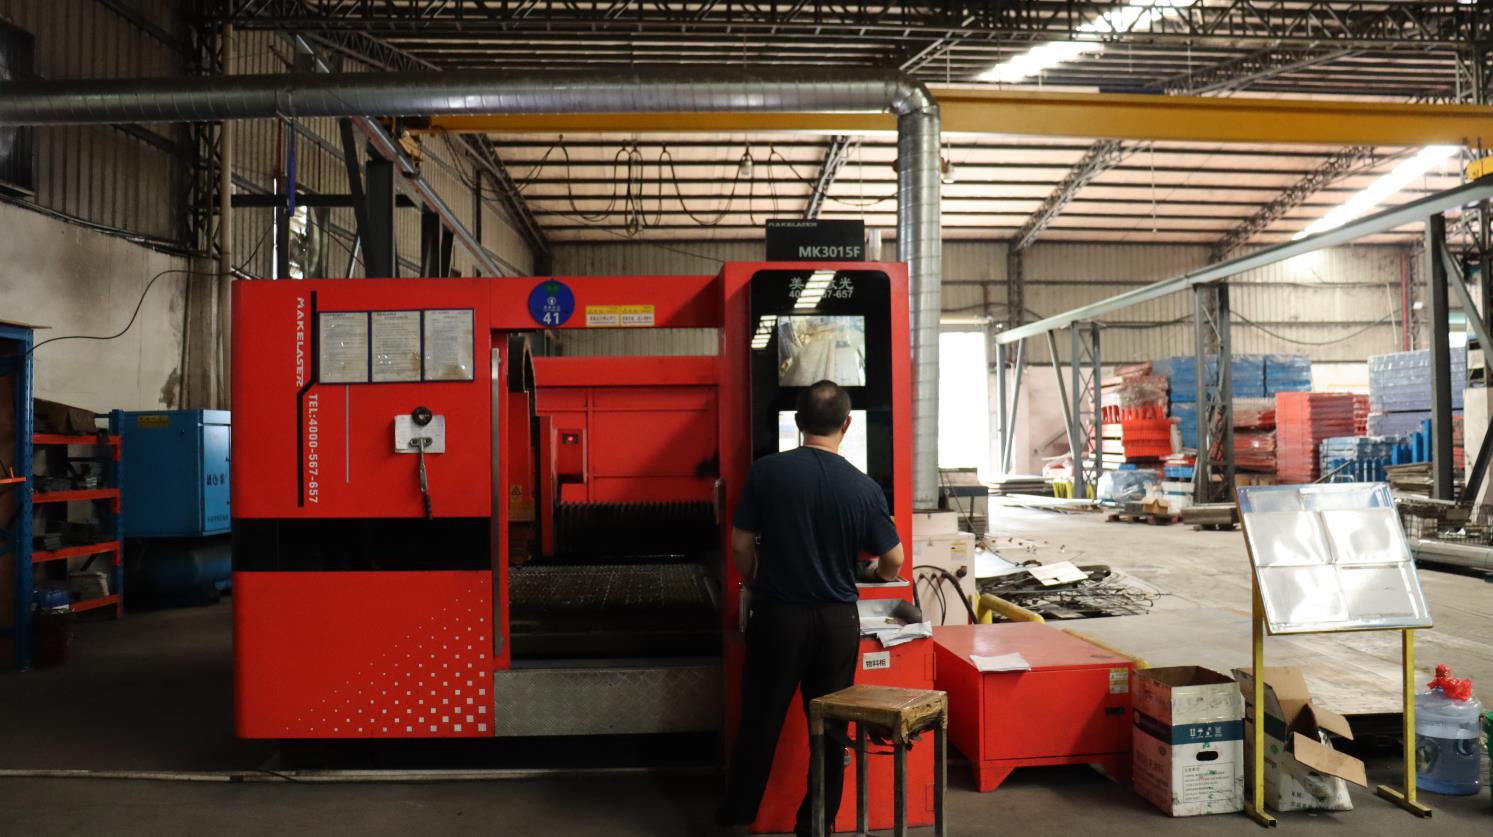
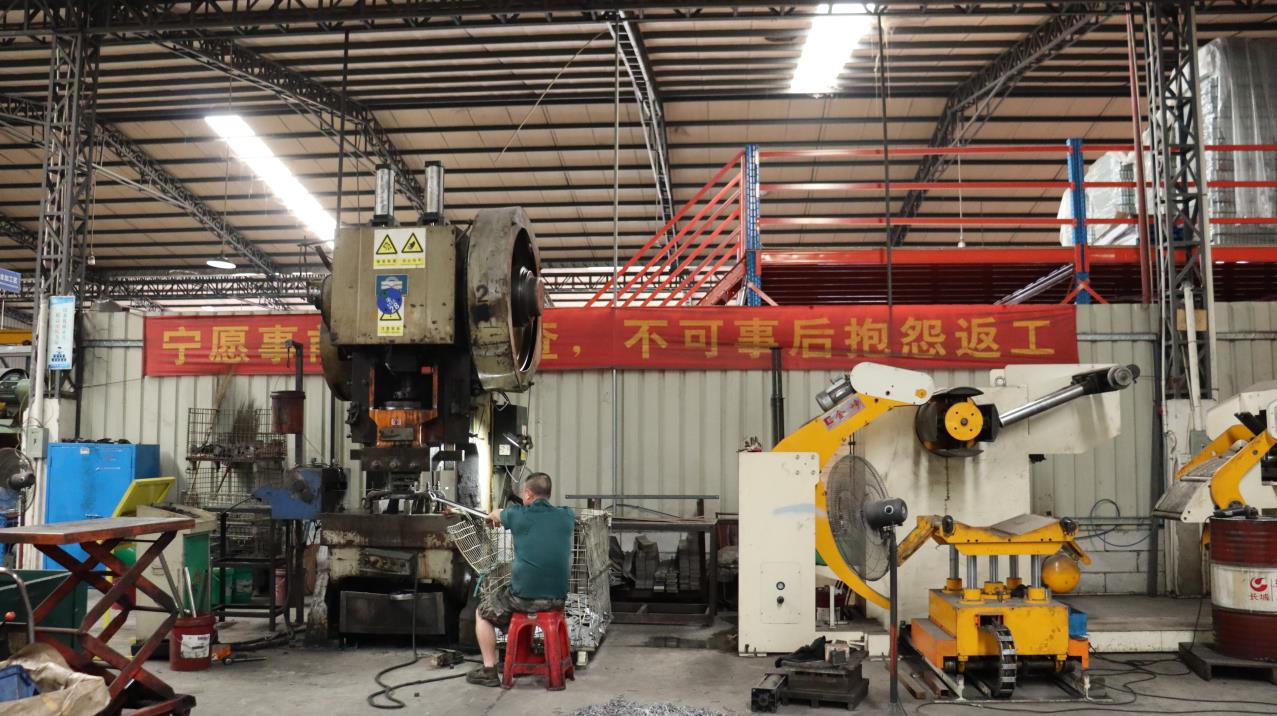
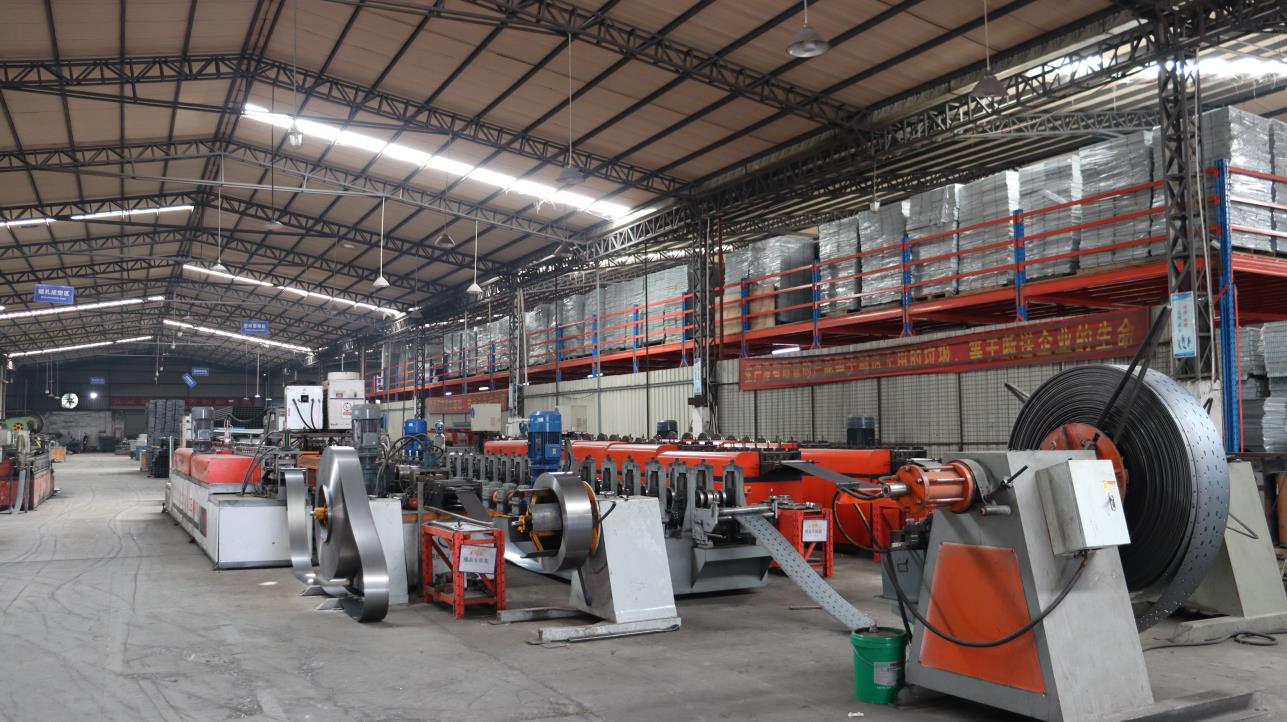
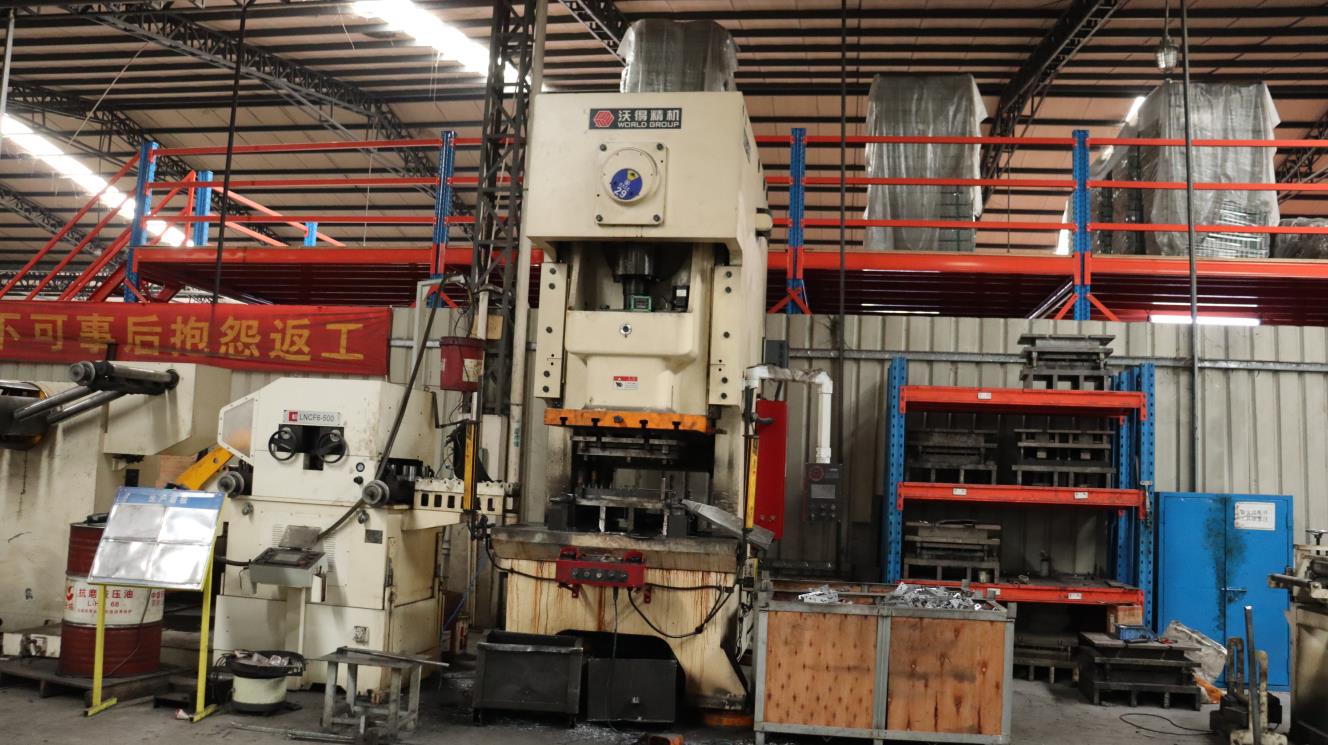
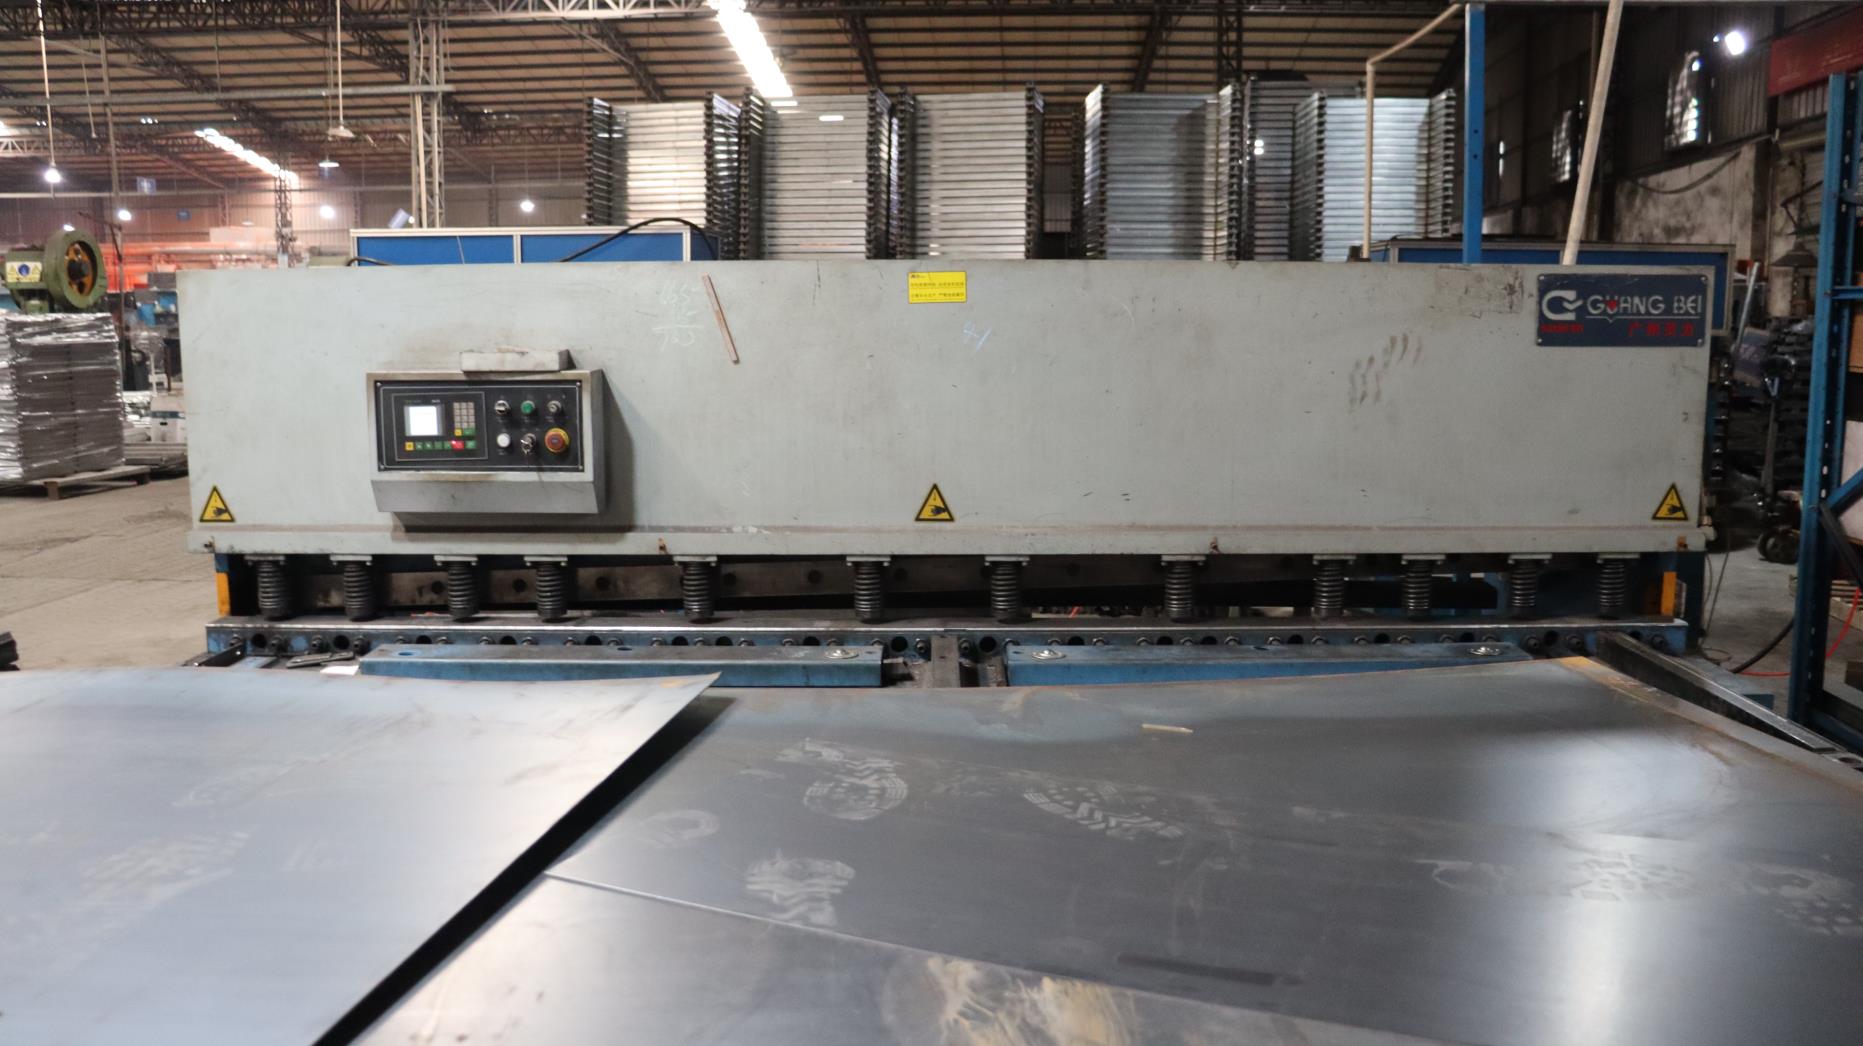
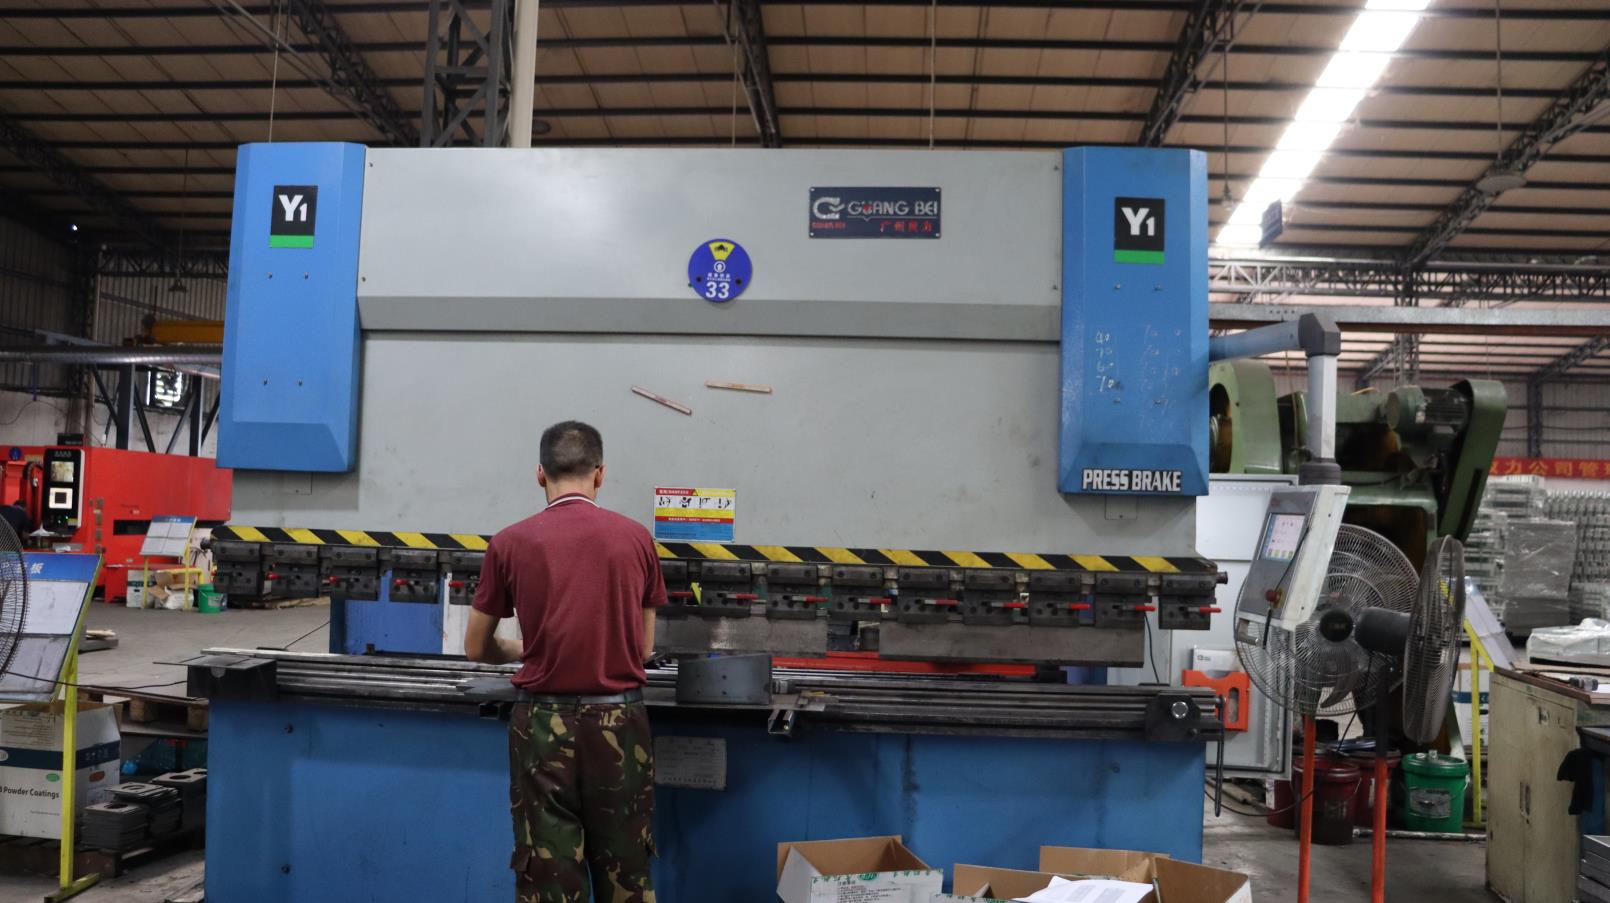
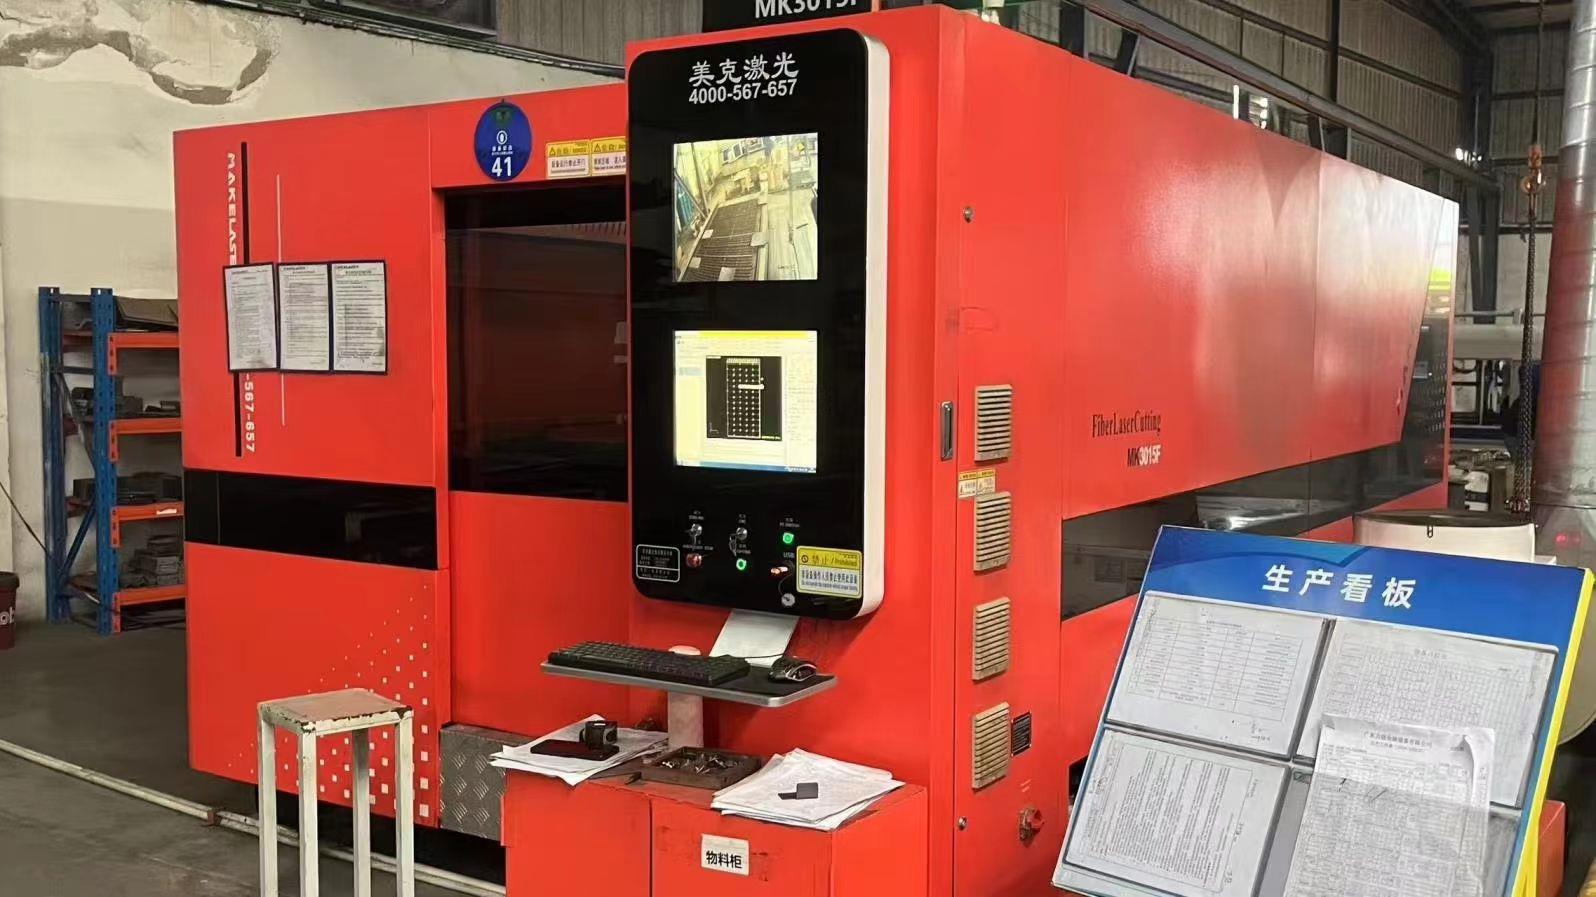
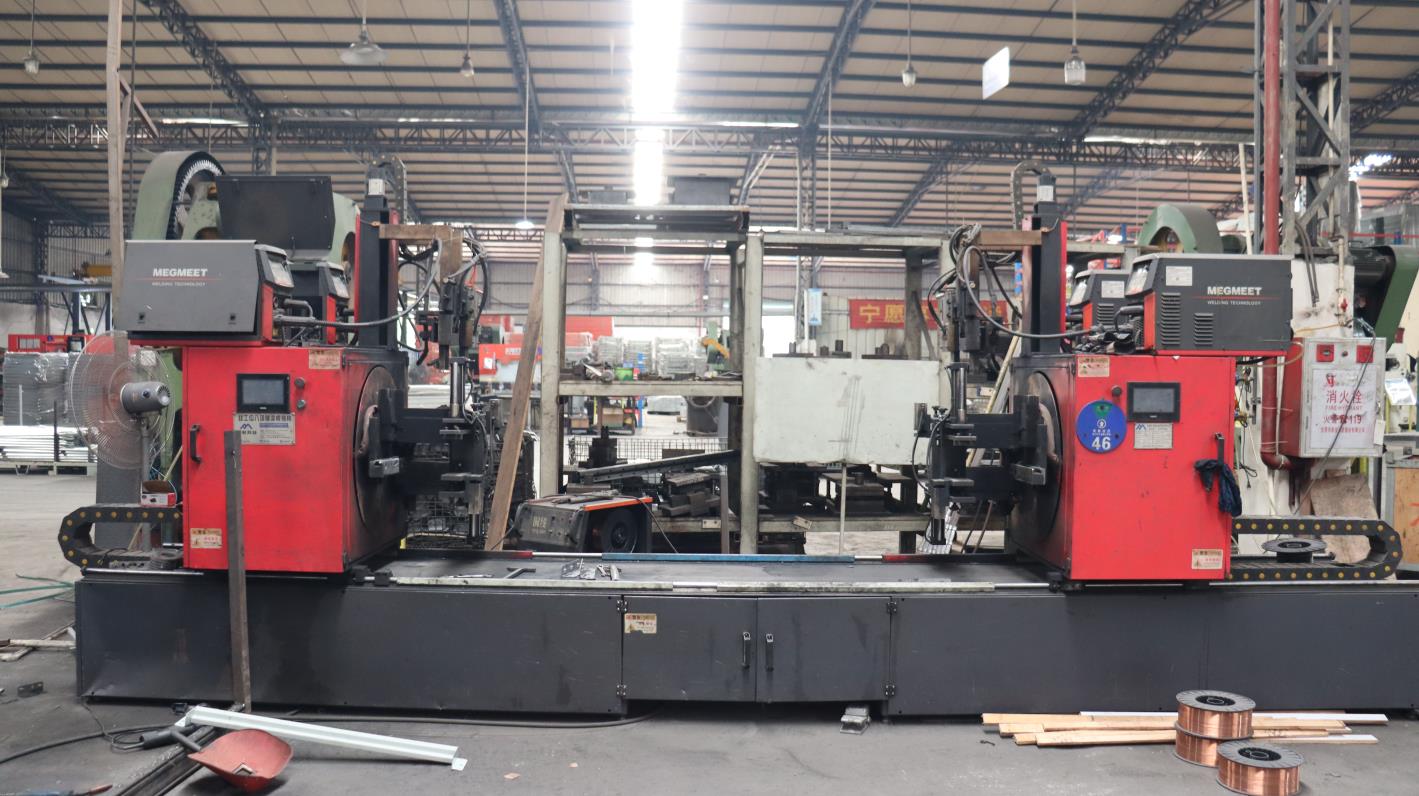
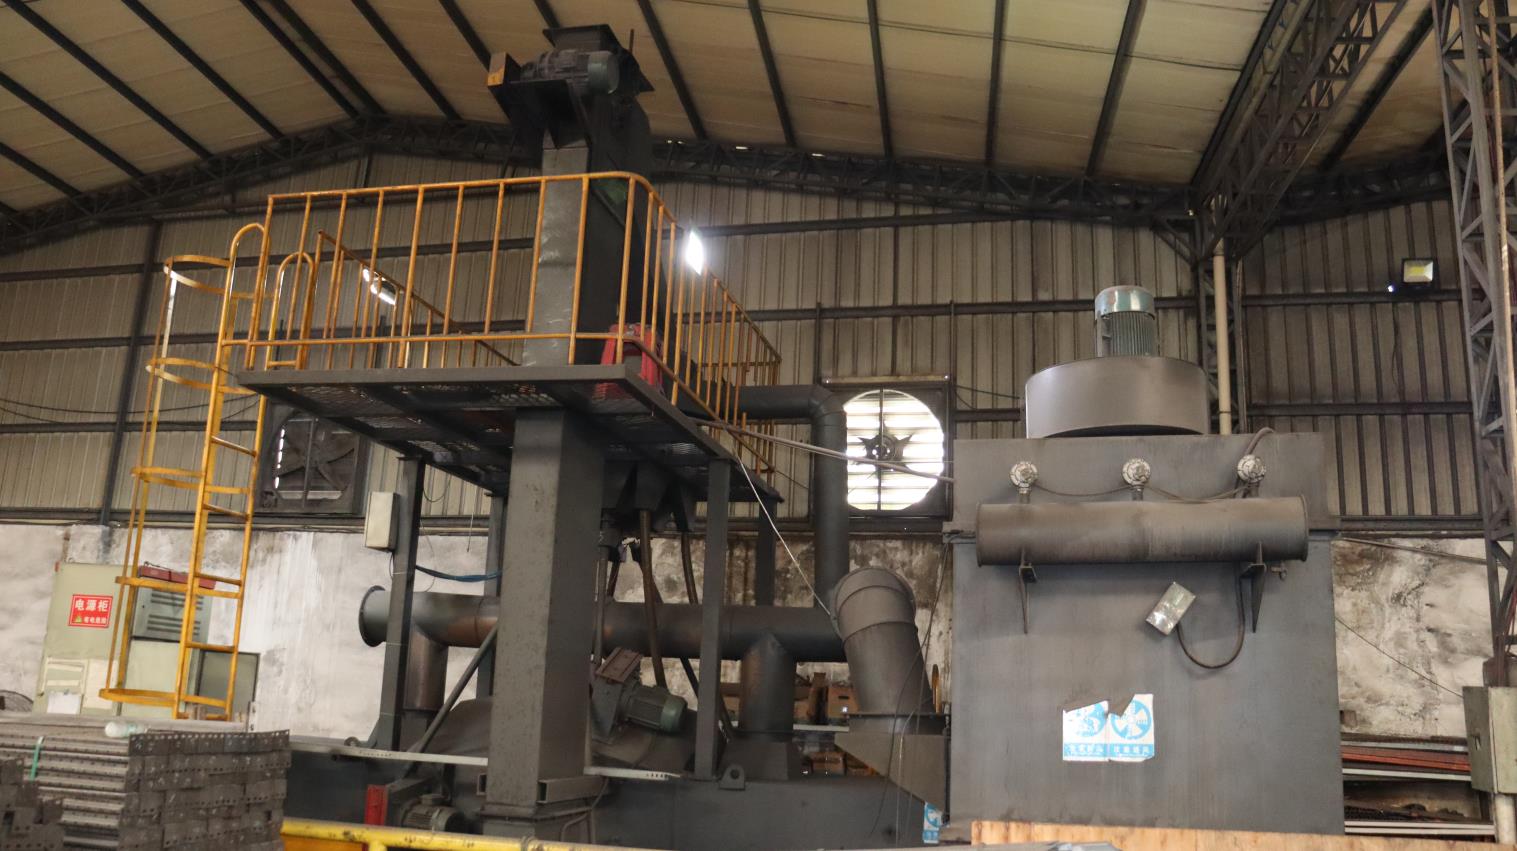
Witness our state-of-the-art production lines, precision CNC machinery, automated robotic welding, and electrostatic powder coating systems.
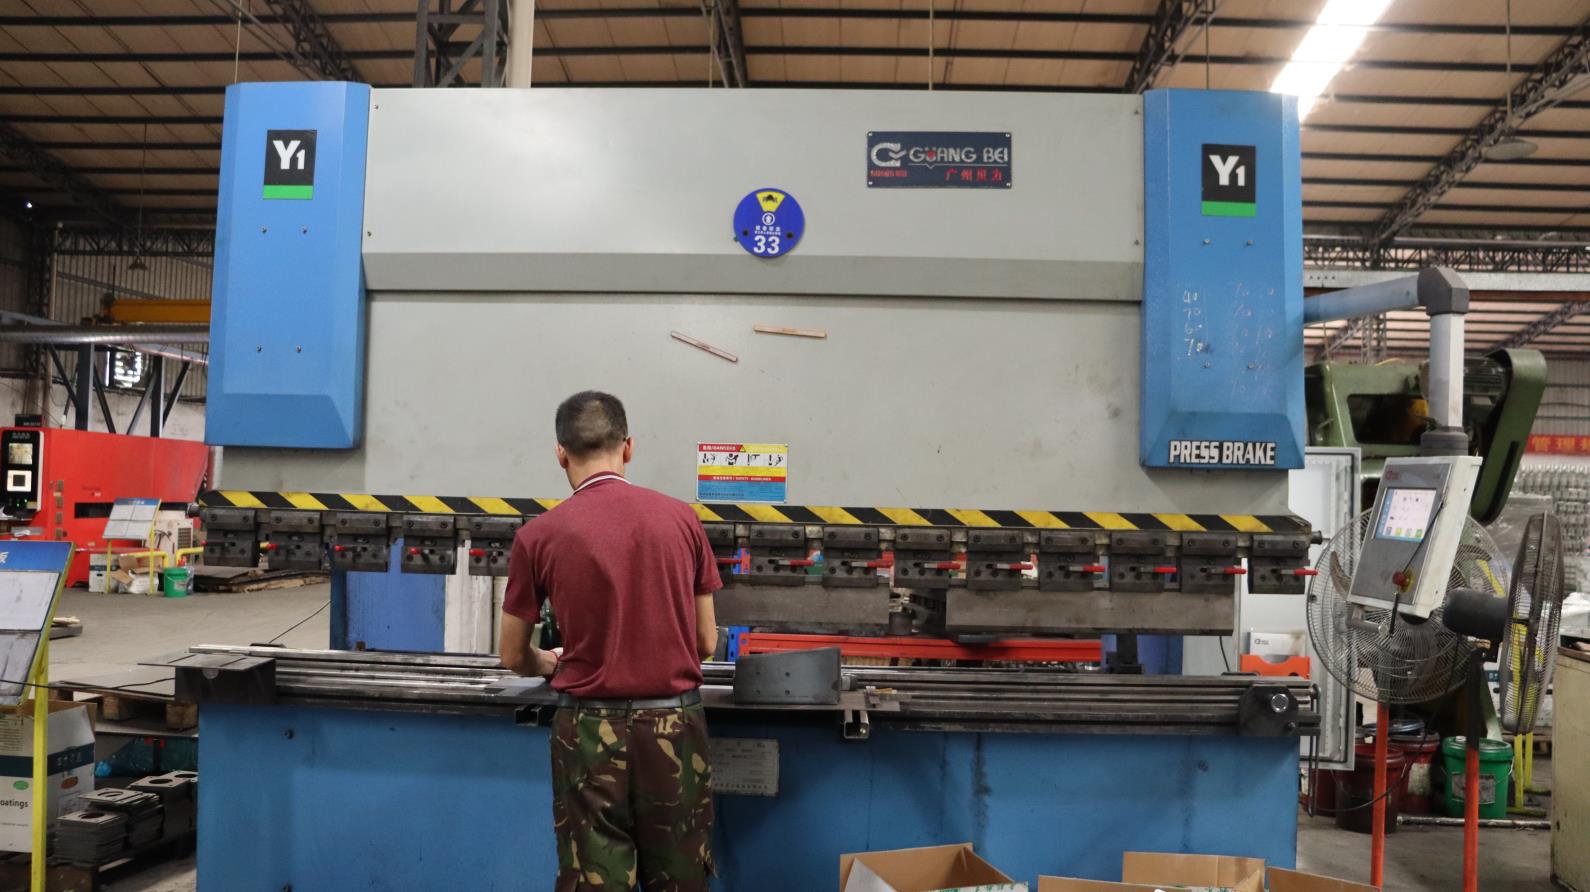
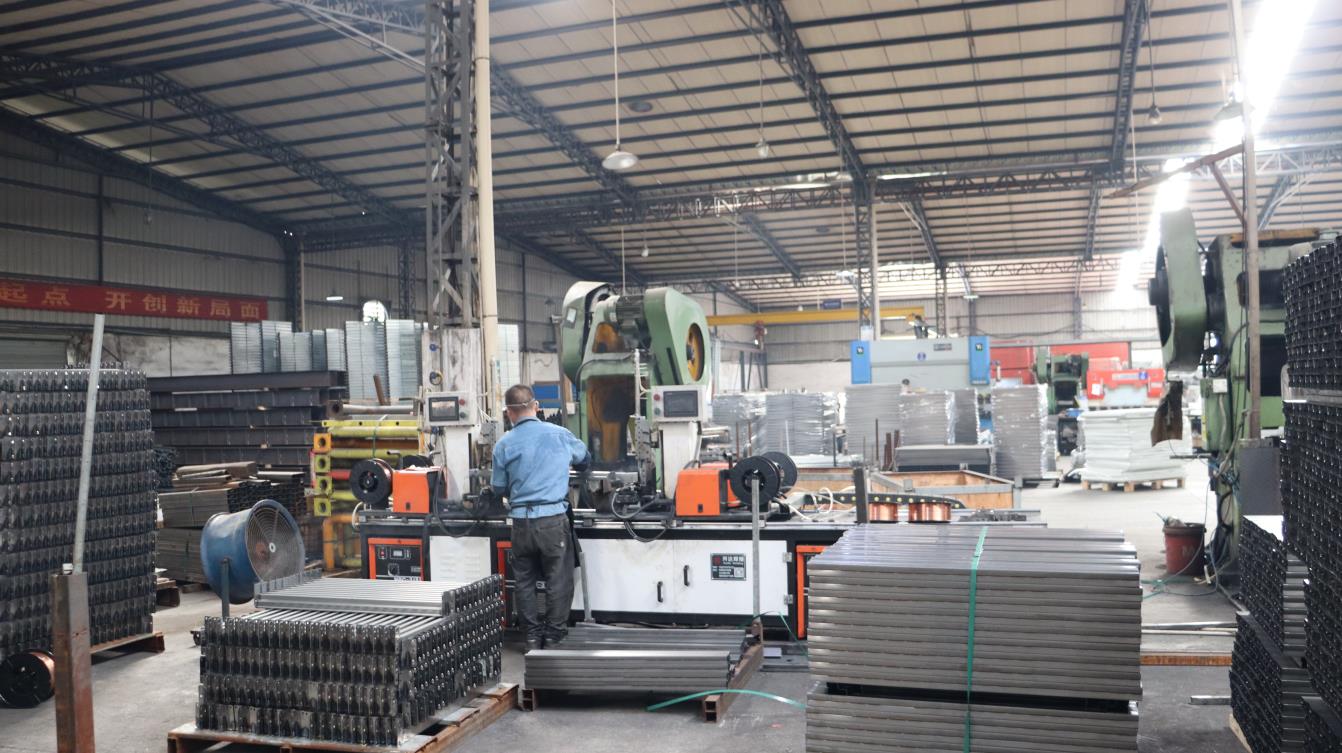
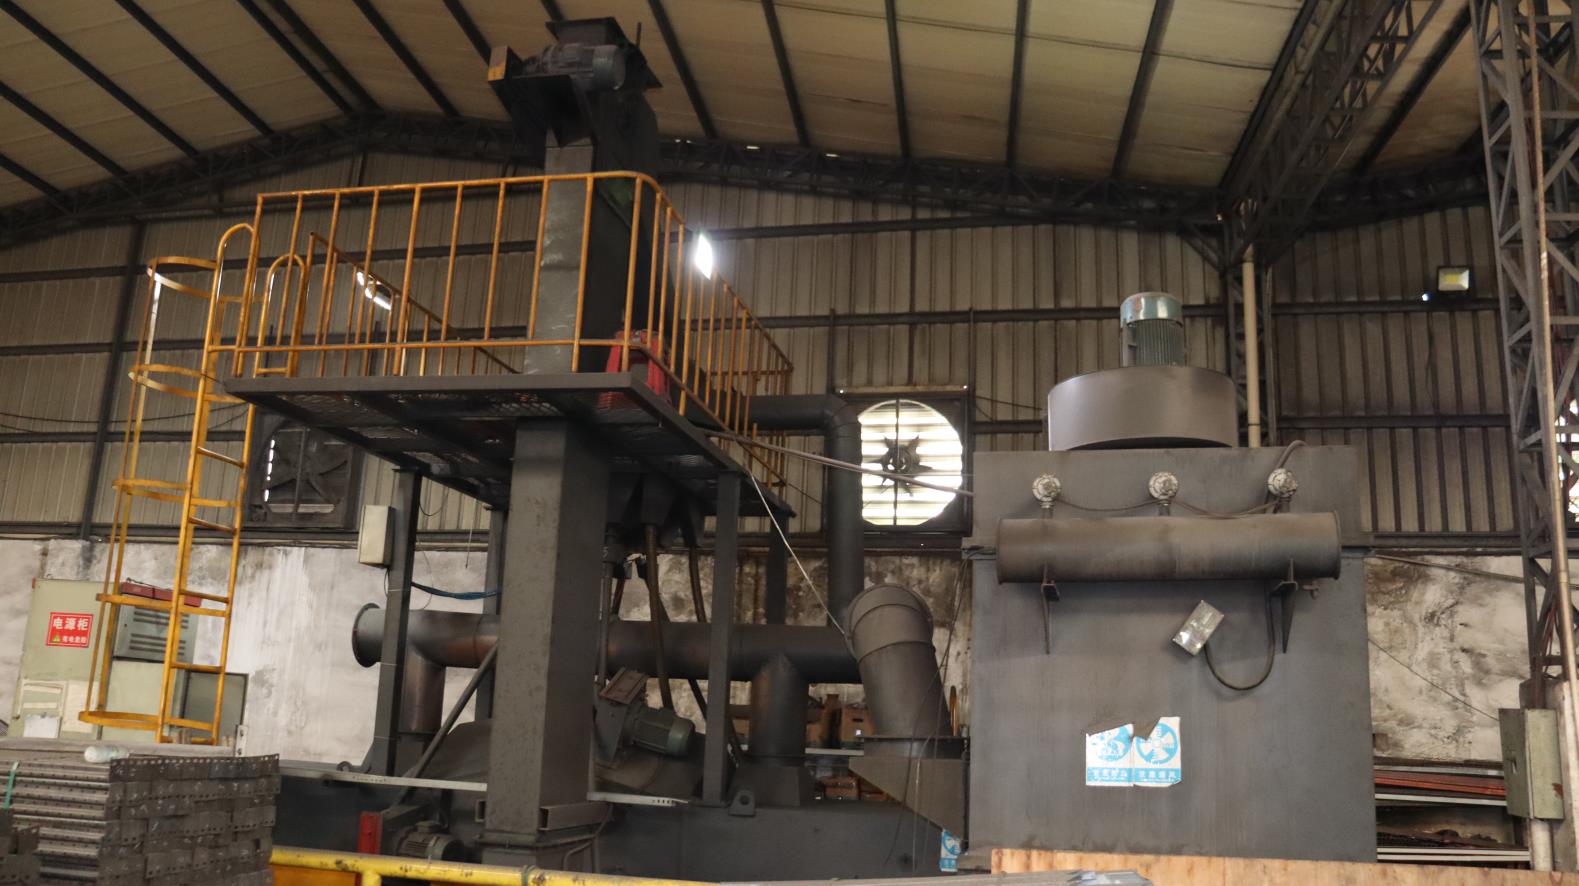
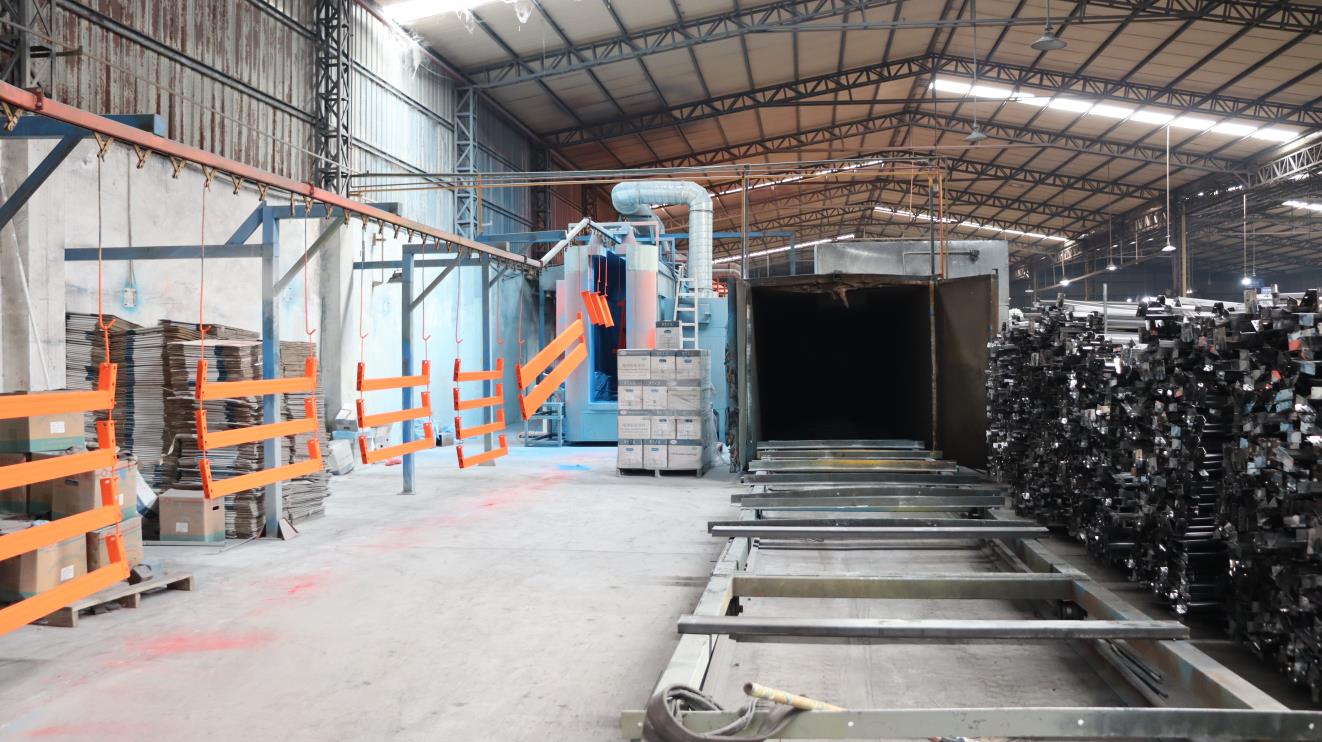
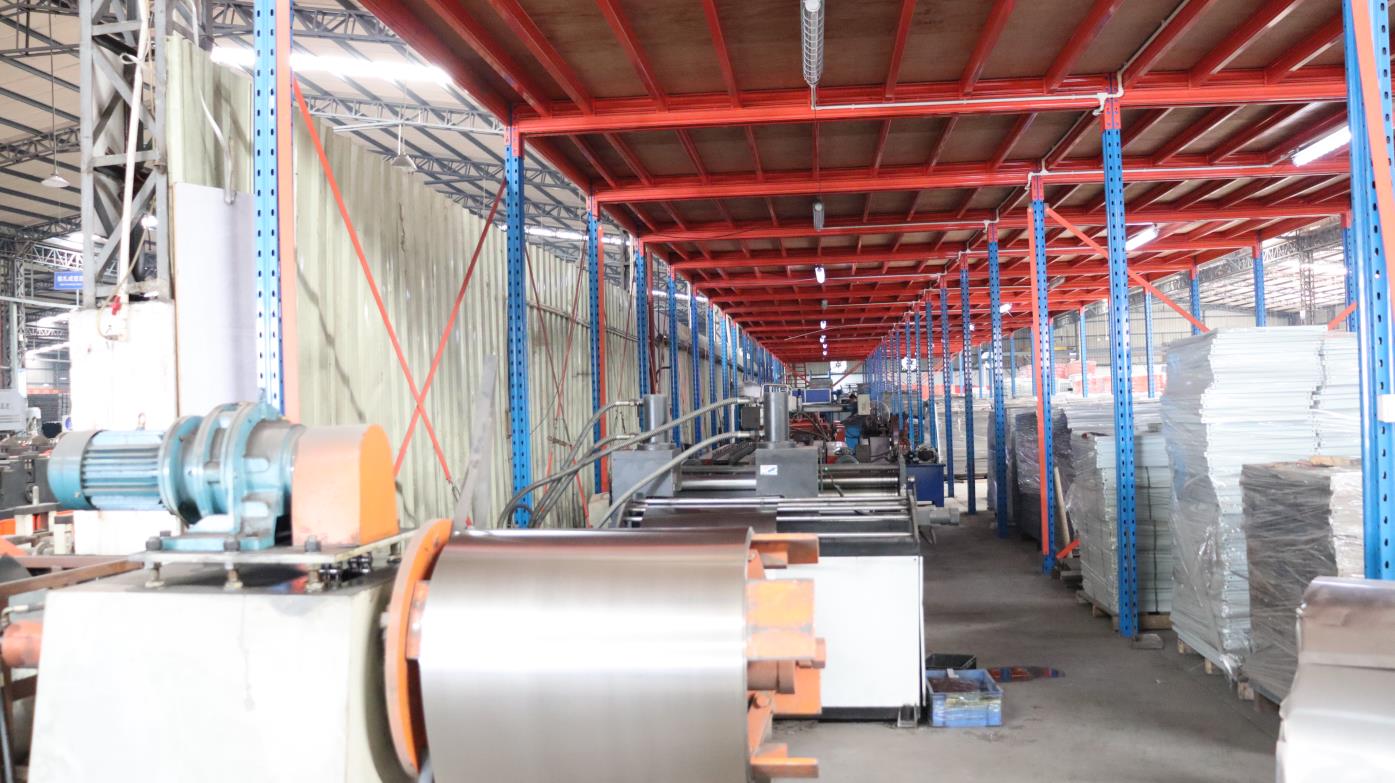
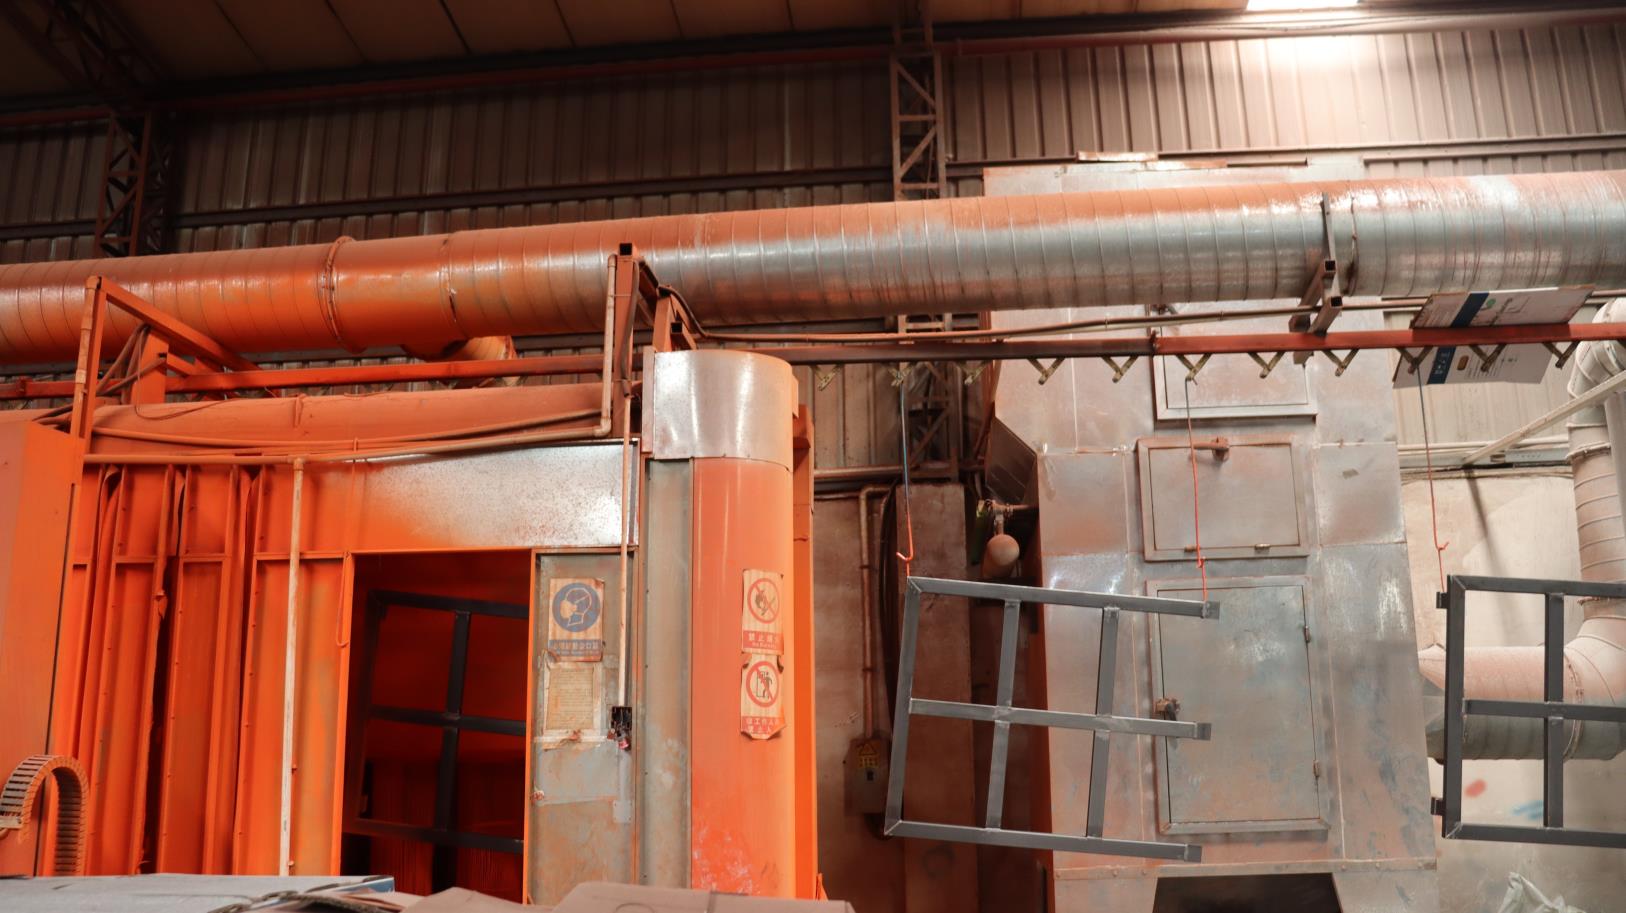
Expert answers regarding wholesale procurement, structural customization, and international shipping of warehouse equipment.
 Lijin Racking